
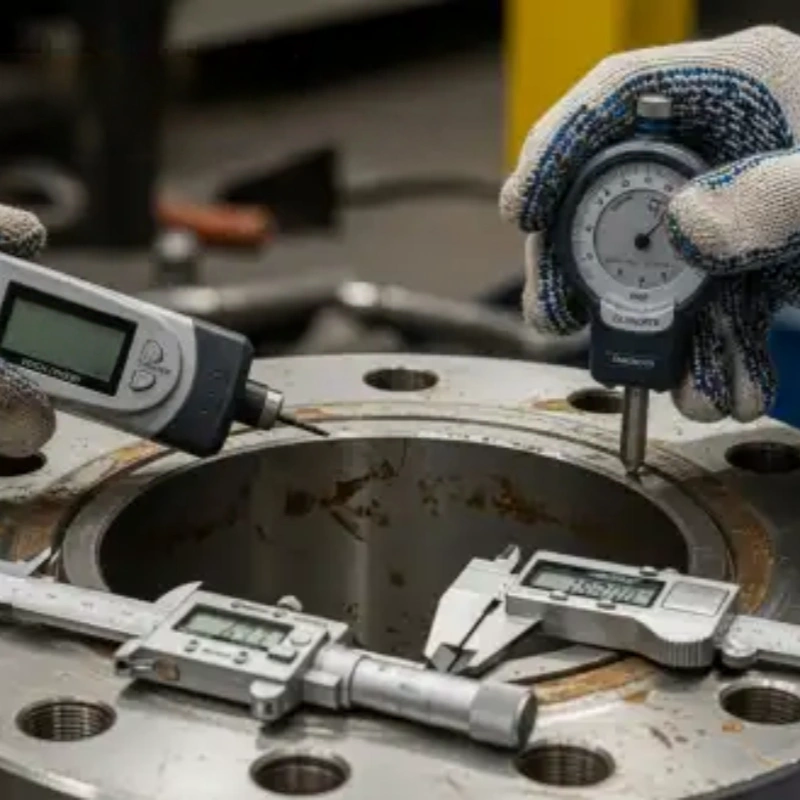
Flange inspection confirms that a new flange or an assembled flanged joint meets the applicable purchase and engineering requirements. Acceptance criteria do not come from a generic web checklist. They come from the purchase order, governing standard and edition, approved drawing, inspection and test plan (ITP), and qualified project procedures.
The first step is to define the inspection stage. Receiving inspection checks the supplied component and its records. Pre-installation inspection checks the mating parts, gasket, and bolting before assembly. In-service inspection assesses the condition of an operating or isolated joint under the owner’s integrity program. Keeping these stages separate produces clearer evidence and a defensible disposition.
Choose the Flange Inspection Stage
| Inspection Stage | Main Question | Typical Evidence |
| Manufacturing or final inspection | Does the finished flange meet the approved product and purchase requirements before release? | Approved drawing, ITP records, certificates, dimensional report, NDT reports, and release note |
| Receiving inspection | Does the delivered item match the purchase order and document package without transport or storage damage? | Marking photographs, certificate match, visual record, measurements, and receiving status |
| Pre-installation inspection | Are both mating flanges, the gasket, fasteners, and assembly conditions correct before tightening? | Joint datasheet, face-condition record, alignment check, component identification, and approved assembly procedure |
| In-service assessment | Is there evidence of leakage, corrosion, movement, or degradation requiring monitoring, repair, or engineering review? | Condition photographs, process history, measurements, inspection results, and risk-based disposition |
The rest of this flange inspection checklist can be adapted to the selected stage. Do not mark a line item “acceptable” until the acceptance reference is identified.
Document Review Checklist
Start with documents because a visually sound flange can still be the wrong product. Confirm the latest approved revision and trace each report to the applicable item or heat number.
- Purchase order, datasheet, and approved drawing revision
- Applicable product or dimensional standard and required edition
- Inspection and test plan with completed hold and witness points
- Material test report with heat number and specified material designation
- Heat-treatment record when required by the purchase specification
- NDT procedure, personnel qualifications, and examination report when NDT is specified
- Dimensional inspection report with units, tolerances, and calibrated instrument identification
- Coating, preservation, pressure-test, or other applicable records when specifically required
- Certificate of conformity, release note, and document index
For API equipment, verify the applicable API flange requirements instead of assuming that a general ASME checklist applies. The governing purchase specification decides which records are mandatory.
Identification and Traceability
Compare the physical marking with the purchase order, drawing, and certificate package. Record the manufacturer, heat or trace number, material designation, size or bore, pressure rating or class, governing standard, flange type, facing or ring-groove identification, and coating or preservation status.
If a marking is missing, unreadable, or inconsistent, quarantine the item for document review rather than reconstructing its identity from appearance.
Use the dedicated guide to verify flange markings and traceability. Marking supports traceability but does not replace material verification or dimensional inspection.
Flange Visual Inspection
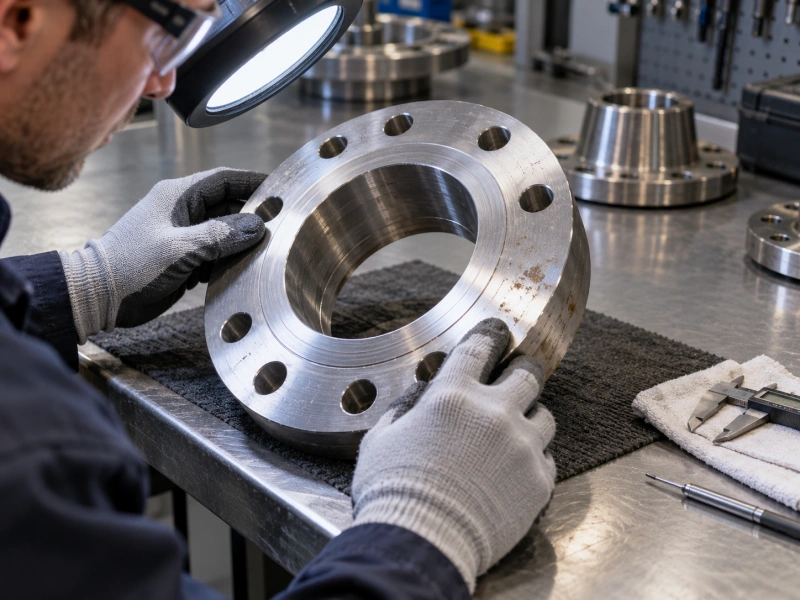
Perform visual inspection under adequate lighting after the accessible surfaces have been cleaned sufficiently for evaluation. Record the location and extent of each indication rather than using only “pass” or “fail.”
| Area | Check For | Record |
| Flange body and hub | Cracks, laps, folds, dents, gouges, corrosion, arc strikes, repair evidence, or handling damage | Location, orientation, length, width, and depth where measurable, plus photographs |
| Bore and transition | Mechanical damage, corrosion, obstruction, and visible profile mismatch | Clock position, axial location, affected area, and drawing reference |
| Bolt holes and threads | Damage, burrs, corrosion, contamination, and blocked access | Hole or stud position, condition, and required disposition |
| Sealing face or groove | Scratches, dents, pits, corrosion, raised metal, coating, or embedded debris | Gasket contact zone, indication direction, dimensions, and photograph reference |
| Coating and preservation | Breakdown, incomplete coverage, contamination, or damage near controlled surfaces | Affected area, coating requirement, and repair status |
Visual testing identifies visible surface conditions; it does not establish material grade or detect every subsurface discontinuity. Any acceptance decision must cite the applicable drawing, standard, purchase requirement, or approved repair procedure.
Flange Dimensional Inspection
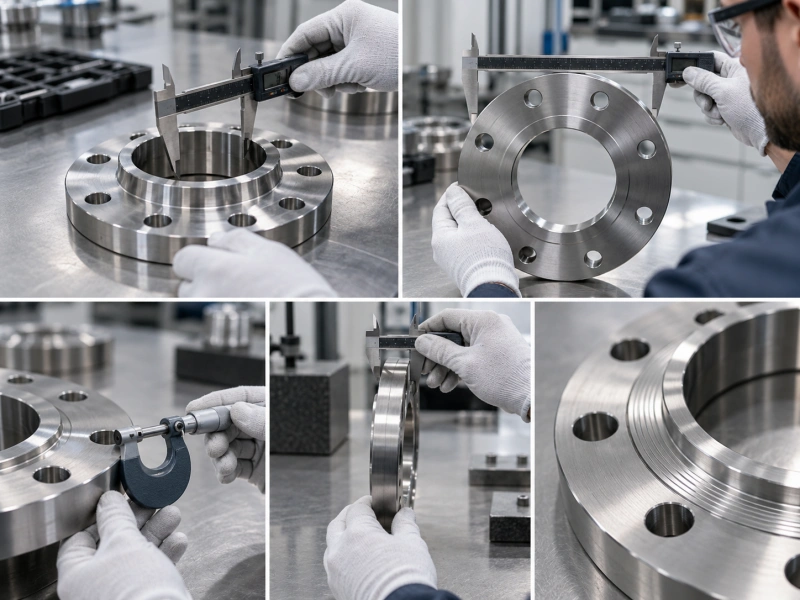
Select the required measurements based on the flange type and approved drawing rather than applying one universal checklist. The following dimensions and features are commonly checked for new flanges and mating-interface verification. The site’s flange face, bore, and bolt hole terminology page can help identify these features, but the approved drawing supplies the values and tolerances.
| Measurement | Typical Tool or Method | Acceptance Reference |
| Outside diameter and bore | Caliper, micrometer, bore gauge, or approved template | Approved drawing and governing dimensional standard |
| Flange thickness and hub profile | Micrometer, caliper, height gauge, or profile measurement | Drawing dimensions and tolerances |
| Bolt circle and hole pattern | Coordinate measurement, approved template, or calculated measurement from hole centers | Drawing, standard table, and mating-component pattern |
| Hole diameter and thread features | Plug or thread gauges, caliper, and visual examination | Drawing and approved thread specification |
| Face flatness and alignment | Straightedge, feeler gauge, dial indicator, or approved metrology method | Project procedure, drawing, or applicable assembly guidance |
| Facing finish | Suitable comparator or specified surface-measurement method | Specified facing requirement and approved inspection method |
| Ring-groove geometry | Approved groove gauge or dimensional measurement suitable for the profile | Connection drawing, ring designation, and governing standard |
Record the actual measured value, not only the result. Include units, instrument ID, calibration status, drawing revision, and the specific acceptance limit.
Flange Face Inspection
The sealing face requires its own record because the effect of a defect depends on the gasket contact area, defect location and direction, joint design, and applicable acceptance criteria. Clean the face using an approved method that does not alter the finish.
- Identify the face type or ring groove and the specified gasket or ring.
- Mark the gasket contact zone on the inspection sketch or photograph.
- Record each scratch, pit, dent, raised area, or corrosion indication by clock position.
- Measure length, width, and depth where the procedure requires it and the method is suitable.
- Note whether an indication runs radially across the sealing path or remains outside the contact zone.
- Assign a disposition—accept, repair, replace, or refer for engineering review—only against a cited requirement.
Do not copy an acceptance depth from another flange type or an unidentified edition of a standard. If the applicable criterion cannot be confirmed, the result remains pending engineering review.
Flange NDT Methods
NDT methods are selected based on the material, manufacturing stage, suspected discontinuity, geometry, and purchase requirements. The method does not set its own acceptance criteria; the approved procedure and governing specification do.
| Method | Useful For | Key Boundary | Required Output |
| VT | Visible surface condition, workmanship, and accessible joint features | Limited to visible and accessible conditions | Visual report, location map, and photographs |
| PT | Surface-breaking indications on clean, nonporous materials | Surface preparation and geometry affect sensitivity; indications require evaluation | Procedure, consumables, dwell conditions, indication record, and disposition |
| MT | Surface and near-surface indications in ferromagnetic materials | Not applicable to nonferromagnetic materials; field direction and surface condition matter | Technique record, equipment checks, indication map, and evaluation |
| UT | Internal discontinuities, thickness measurement, or selected near-surface examinations | Geometry, grain structure, access, calibration, and procedure determine capability | Calibration record, scan coverage, indication data, and evaluation |
| RT | Volumetric examination where geometry and defect orientation suit the technique | Radiation controls, access, and image geometry require a qualified plan | Technique sheet, images, coverage record, and interpretation |
Use qualified personnel and calibrated equipment as required by the project. The inspection plan should state the examination extent, technique, acceptance reference, reporting level, and treatment of relevant indications.
Pre-Installation Bolted Joint Inspection
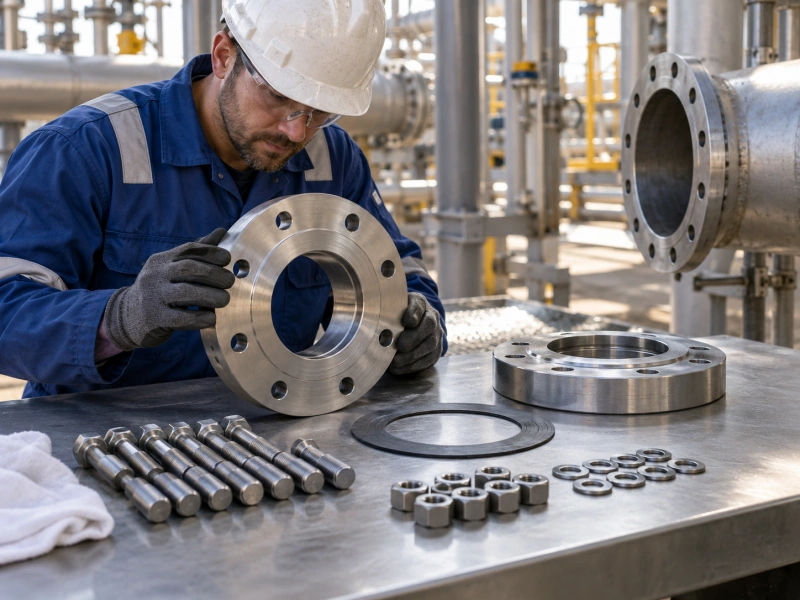
Before assembly, confirm that the two flanges belong to the intended joint and that their faces, gasket, and fasteners match the approved joint specification. Check alignment, accessible damage, cleanliness, gasket identification, fastener identification, lubrication requirements, and tool calibration.
Use the project-approved bolted-joint assembly procedure for the tightening sequence, target bolt load or torque, tightening passes, and completion records. This page does not publish universal torque values or recommend routine retightening. ASME PCC-1 may provide project guidance for pressure-boundary bolted flange joint assembly when the owner’s specification makes it applicable.
Pressure and Leak Testing Boundary
A dimensional or visual flange inspection is not automatically a pressure test. Component or system testing may be specified after manufacturing, assembly, or repair, but the test medium, pressure, duration, boundaries, instrumentation, acceptance criteria, and safety controls must come from the governing code and an approved test procedure.
Do not apply a fixed percentage of operating pressure from a general article. Pneumatic or gas testing involves stored-energy hazards and requires project authorization, isolation, exclusion controls, and qualified personnel. Record the test reference and report when testing is part of acceptance; otherwise mark it “not specified,” not “passed.”
In-Service Flange Inspection
In-service inspection evaluates the assembled joint within the owner’s integrity-management program. Review the operating temperature and pressure history together with evidence of leakage, corrosion products, coating breakdown, fastener degradation, movement, vibration effects, and insulation deterioration.
The inspection interval and method should follow risk-based planning, service severity, degradation mechanisms, operating history, regulatory requirements, and previous findings. Do not use an unsupported six-month or annual interval. The separate guide to in-service flange inspection planning covers maintenance decisions without duplicating this acceptance checklist.
Flange Inspection Record Template
Use one record per flange or joint when individual traceability is required. Attach marked-up photographs and measurement sheets rather than compressing important evidence into a single comment field.
| Record Field | Entry |
| Asset or item ID | Equipment tag, line number, purchase item, or joint ID |
| Inspection stage | Final, receiving, pre-installation, or in-service |
| Reference documents | PO, drawing revision, standard edition, ITP, and procedure |
| Identification | Manufacturer, heat number, material, size, rating or class, and facing |
| Inspection item | Document, marking, visual, dimensional, face, NDT, bolting, or test record |
| Actual result | Measured value or observed condition with units and location |
| Acceptance reference | Drawing dimension, specification clause, or approved criterion |
| Status | Accept, hold, repair, replace, or engineering review |
| Evidence | Photo number, report number, and instrument ID |
| Approval | Inspector, date, reviewer, and disposition approval |
Inspection Evidence for API Flange Procurement
For an API flange quotation, define the inspection evidence before purchase. State the drawing approval process, material traceability, dimensional report, required NDT, test records, coating documents, and final document package. Use the API flange material documentation guide to verify the applicable material records and traceability requirements.
AlienFrac performs API flange inspection and provides the agreed documentation in accordance with the customer datasheet and inspection scope. See our guide to final inspection after flange manufacturing for an overview of where inspection fits within the production process. Confirm the exact inspection plan and deliverables in the quotation instead of assuming every method applies to every flange.
Send the flange specification, drawing, inspection and test plan, quantity, and required document package through our Contact Us page to request a product review or quotation.
FAQ
What Is Included in a Flange Inspection?
The scope may include document review, marking and traceability, visual inspection, dimensional measurement, sealing-face evaluation, specified NDT, pre-installation joint checks, and review of required test records. The purchase specification decides which items apply.
Which Flange Dimensions Should Be Measured?
Common checks include OD, bore, thickness, hub dimensions, bolt circle, hole diameter, thread features, flatness, facing finish, and ring-groove geometry. Select the fields and tolerances from the approved drawing and governing standard.
Which NDT Method Is Best for a Flange?
There is no universal best method. Select VT, PT, MT, UT, or RT according to material, suspected discontinuity, geometry, manufacturing stage, access, and the governing requirement.
Can a Flange Pass Visual Inspection but Fail Acceptance?
Yes. It may have incorrect dimensions, material grade, markings, documentation, or hidden discontinuities even when the visible surface appears acceptable. Final acceptance requires all specified inspection requirements to be satisfied or formally dispositioned in accordance with the governing procedure.
How Often Should In-Service Flanges Be Inspected?
Set the interval through the owner’s risk-based inspection or integrity program. Service conditions, degradation mechanisms, consequences of failure, operating history, regulatory requirements, and previous findings all affect the inspection frequency.
What Should Be Included in an Inspection Report?
Include item identity, inspection stage, reference documents, actual observations or measurements, acceptance criteria, equipment and calibration data, photographs, report references, status, inspector, date, and approved disposition.
Reference Guidance
Use the editions required by the purchase order and project specification. Official information is available for ASME PCC-1 and API Specification 6A. Controlled standards, approved drawings, and project procedures take precedence over this general checklist.